Scratches, cracks, chips and surface discontinuities
Use raking, diffuse, bright-field or dark-field illumination as the surface demands, then validate the defined discontinuities across material, finish, tooling and supplier variation.

Metals and machining
Evaluate surfaces, presence, orientation and optically measurable conditions with qualified plant cameras, factory-owned edge inference and a customer-chosen cloud account.
The right architecture depends on the visual signal, process risk, line conditions and validation standard, not the industry label alone.
Candidate inspection families
These are categories to evaluate, not claims of deployed performance.
Use raking, diffuse, bright-field or dark-field illumination as the surface demands, then validate the defined discontinuities across material, finish, tooling and supplier variation.
Confirm that holes, slots, inserts, threads or other visible features are present and oriented correctly while fixtures hold the part within the qualified view.
Measure configured edges, gaps or positions only when calibration, lens distortion, working distance, focus and part presentation can be controlled to the required tolerance.
Use visible residue, tool marks, orientation or handling evidence to support a defined decision; do not ask the model to infer a condition the image cannot show.

Readiness
A credible review covers optics, lighting, field of view, product presentation, cycle time, edge compute, interfaces, response and acceptance criteria.
Use Cases
Each use case connects the inspection workflow to the questions a plant should answer before production deployment.
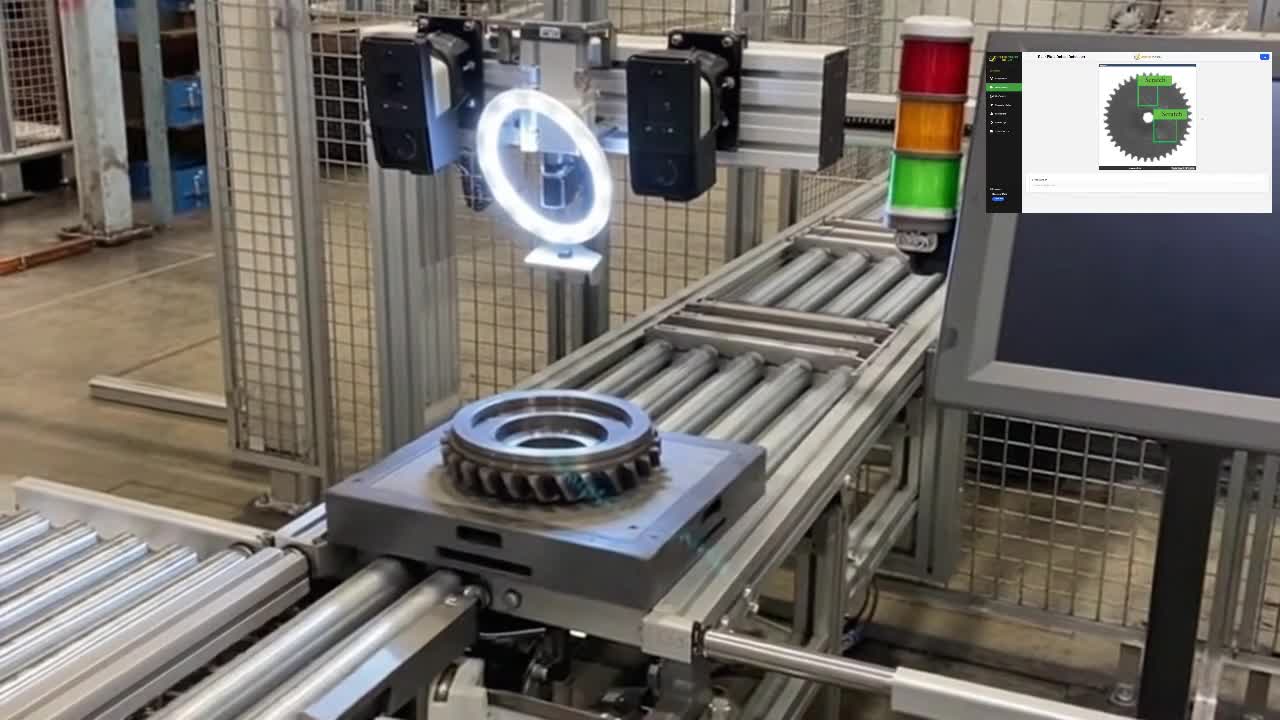
A workflow for learning the appearance of acceptable surfaces and configured discontinuities.
Review the workflow
A workflow for estimating configured dimensions when optics, calibration and part presentation are controlled.
Review the workflow
A workflow for identifying visible or fluorescent evidence on a component before it moves downstream.
Review the workflowQuestions answered
Choose a visible, economically relevant condition with accessible images, a clear decision, manageable integration and a practical validation set. The best first use case proves the complete operating workflow.
Not safely by default. Cameras, lighting, products, fixtures, suppliers and process conditions can differ. Reuse the deployment package and governance, then validate locally.
No. Stable, deterministic checks can remain an excellent fit for traditional machine vision. United Vision should be evaluated where learned visual patterns and a reusable plant-owned lifecycle are useful.
Yes, when the existing equipment is suitable and supported for the inspection. The review qualifies image quality, optics, lighting, timing, interfaces, edge capacity and the plant environment; United Vision does not require one proprietary camera and edge stack.
Production inference always runs on a supported factory-owned edge device. United Vision cloud services run in a supported cloud account chosen and owned by the customer, keeping the real-time decision close to the line.
Yes. One factory license supports unlimited United Vision use cases within the licensed factory. Each use case still requires suitable evidence, imaging, integration and production validation.
Bring the product, image source, process condition, decision and current inspection method. We will use those facts to test fit.